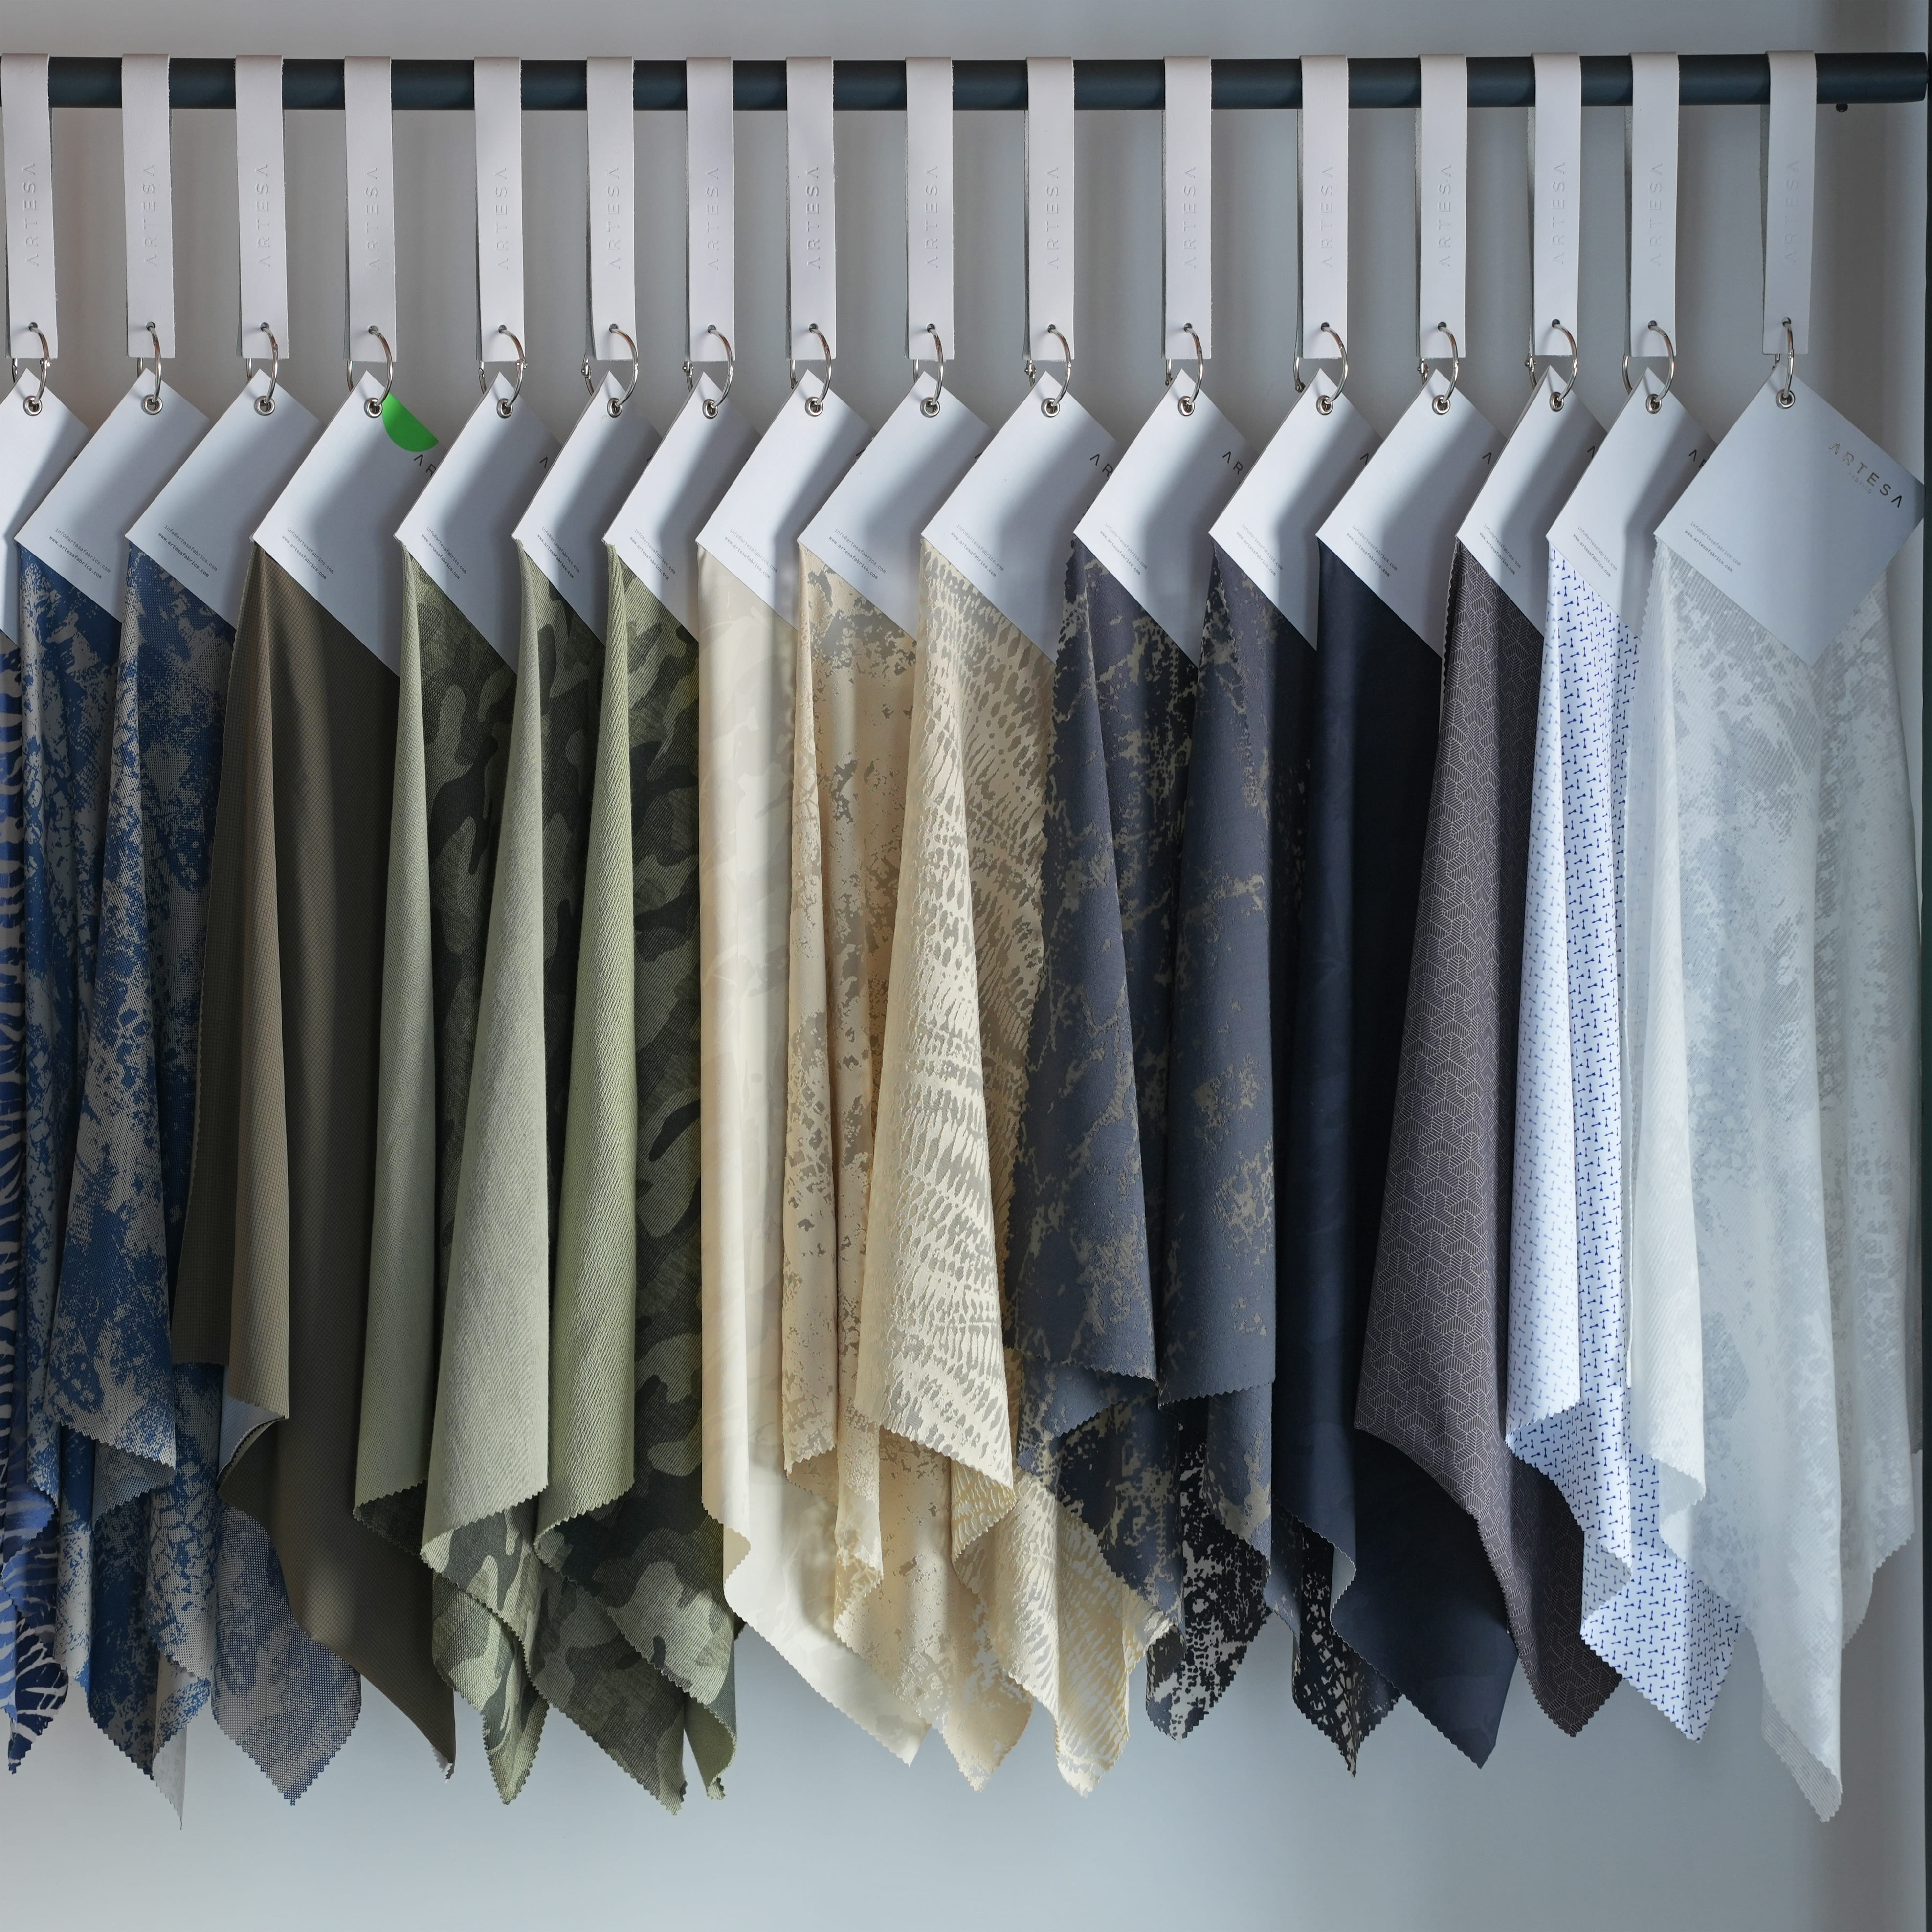
Sustainable clothing manufacturing aims to reduce the environmental and social impacts of apparel production through the use of environmentally responsible materials, ethical labor practices, efficient resource management and waste reduction techniques.
Every stage of production matters, from raw material sourcing and fabric development to dyeing, finishing and energy consumption. However, sustainability is not determined by fabric selection alone. Manufacturing methods, working conditions, garment durability and supply chain transparency must also be considered.
This guide explores the materials used in sustainable clothing manufacturing, key production methods, environmental improvement practices and important textile certifications.
What Is Sustainable Clothing Manufacturing?
Sustainable clothing manufacturing refers to producing garments using practices designed to reduce environmental and social impacts through responsible material sourcing, resource efficiency, waste reduction and ethical production.
The key pillars of sustainable manufacturing include:
- Sustainable materials: Using organic, recycled or responsibly sourced fibers and fabrics.
- Low-impact dyes and treatments: Evaluating technologies that can reduce water, energy and chemical consumption.
- Waste minimization: Improving fabric cutting efficiency, material reuse and recycling.
- Energy and water efficiency: Monitoring resource consumption and implementing suitable improvements.
- Fair labor and ethics: Supporting workers' rights, safe workplaces and responsible employment practices.
- Responsible chemical management: Controlling environmental and health risks associated with chemicals used during textile manufacturing.
Considering these elements together helps manufacturers establish more responsible apparel production processes.
Why Is Sustainable Clothing Manufacturing Important?
The textile and apparel industry has environmental impacts across raw material production, dyeing, finishing, energy consumption and textile waste management.
Reducing resource consumption and improving manufacturing processes are important steps toward managing these impacts.
For fashion brands, sustainable clothing manufacturing can offer several benefits:
- Reduced environmental impacts: Improving the efficiency of energy, water and raw material use.
- Better product quality: Selecting suitable materials and manufacturing methods to support garment durability.
- Greater supply chain transparency: Improving access to reliable information about material origins and production processes.
- Responsible sourcing: Evaluating environmental and social requirements across manufacturing partnerships.
Meaningful progress depends on measurable improvements throughout manufacturing operations rather than material selection alone.
What Materials Are Used in Sustainable Clothing Manufacturing?
Material selection is an essential part of sustainable apparel manufacturing.
In addition to organic and recycled fibers, manufacturers may consider alternative plant-based materials and responsibly produced cellulosic fibers.
| Material | Characteristics and potential benefits |
|---|---|
| Organic cotton | Produced according to organic agricultural standards that restrict certain synthetic agricultural chemicals. |
| Recycled polyester | Produced from recovered polyester-containing materials and can reduce demand for virgin polyester feedstocks. |
| Recycled cotton | Supports the recovery and reuse of cotton-containing textile waste. |
| Hemp | A plant-based fiber whose environmental performance depends on cultivation and processing conditions. |
| Linen | A natural fiber derived from flax, recognized for its durability and functional characteristics. |
| Lyocell | A cellulose-based fiber that can be manufactured using solvent recovery processes. |
The environmental performance of each material varies depending on cultivation or production methods, energy use, chemical processing and end-of-life management.
Therefore, no single fabric can automatically be considered the most sustainable option for every application.
Key Practices in Sustainable Clothing Manufacturing
Beyond material selection, manufacturing technologies and operational management play important roles in improving sustainability performance.
Low-Impact Dyeing and Textile Treatments
Dyeing, printing and finishing are important stages of textile production involving water, energy and chemical use.
Several technologies can be evaluated to reduce environmental impacts:
- Low-water dyeing: Methods designed to reduce water consumption during textile dyeing.
- Waterless dyeing technologies: Alternative technologies that can significantly reduce water requirements for suitable fibers and dyeing systems.
- Digital textile printing: Methods that can optimize dye, printing paste or material consumption under certain production conditions.
- Enzymatic treatments: Biotechnology-based processes that may provide alternatives to conventional chemical treatments in specific applications.
The environmental benefits of these methods depend on the technology, materials and manufacturing conditions.
Not every method is suitable for all fabric types or production processes.
Waste Reduction and Recycling
Textile waste can be generated during fabric cutting, sampling and garment assembly.
Manufacturers can reduce material waste through digital pattern layouts, optimized cutting plans and regular monitoring of fabric consumption.
Reusing suitable fabric offcuts, separating production waste and working with recycling partners can also support more efficient resource use.
However, preventing waste generation should generally take priority over recycling whenever possible.
Energy and Water Efficiency
Managing energy and water consumption is essential for improving the environmental performance of textile manufacturing.
Manufacturers may consider practices such as:
- Using renewable electricity sources.
- Installing energy-efficient equipment and LED lighting.
- Monitoring water consumption throughout production.
- Evaluating water recovery and reuse systems where appropriate.
- Optimizing equipment maintenance and production planning.
Closed-loop water systems can help recover and reuse a portion of process water in suitable facilities.
However, recovery rates depend on the technology and manufacturing processes involved.
Responsible Chemical Management
Dyes, processing chemicals and finishing agents can create environmental and health risks if they are not properly managed.
Responsible chemical management involves maintaining chemical inventories, ensuring appropriate storage, training employees and meeting relevant environmental requirements.
Systems such as bluesign® support improvements in chemical and resource management throughout textile manufacturing.
Ethical Working Conditions
Sustainable garment manufacturing involves more than environmental management. Workers' rights and workplace safety are also essential components of responsible production.
Safe workplaces, compliance with working-hour regulations, appropriate compensation practices and accessible employee grievance mechanisms are important considerations.
Social compliance assessments and continuous improvement activities can help manufacturers evaluate and strengthen these practices.
Important Certifications in Sustainable Textile Manufacturing
Certifications and management system standards help evaluate manufacturers against defined quality, environmental and social responsibility requirements.
| Certification or system | Main focus |
|---|---|
| GOTS | Environmental and social requirements for certified organic textile processing |
| GRS | Recycled material content and related environmental, chemical and social requirements |
| OEKO-TEX® STANDARD 100 | Testing textile products for specified harmful substances |
| bluesign® System Partner | Partnership in a system focused on responsible chemical and resource management |
| ISO 9001 | Quality management systems |
| ISO 14001 | Environmental management systems |
| ISO 45001 | Occupational health and safety management systems |
| SA8000 | Social accountability and workplace requirements |
These systems address different aspects of responsible manufacturing.
Holding a certification does not automatically mean that all products or activities meet every sustainability criterion.
For example, OEKO-TEX® STANDARD 100 focuses on product testing for specified harmful substances, while ISO 14001 addresses environmental management systems.
Brands should verify certificate validity and the facilities, processes or products covered.
How Does Aster Textile Support Sustainable Clothing Manufacturing?
With roots dating back to 1987 and established in 1993, Aster Textile is a vertically integrated apparel manufacturer working with international fashion brands.
With manufacturing facilities in Türkiye and a new facility in Egypt’s Alexandria Free Zone, Aster Textile combines garment manufacturing expertise with the fabric development capabilities of its group company, Artesa Fabrics.
Guided by its Thoughtful Living vision, the company places quality management, resource efficiency, responsible material sourcing and continuous improvement at the centre of its manufacturing approach.
Aster Textile's Certifications and Sustainability Approach
Aster Textile supports its responsible manufacturing practices through internationally recognized certifications and management system standards, including GOTS, OCS, GRS, RCS, RegenAgri, OEKO-TEX®, ISO 9001, ISO 14001 and ISO 45001.
Together with its fabric mill and dyehouse Artesa Fabrics, Aster Textile became Türkiye’s first fabric-to-garment bluesign® System Partner.
This status reflects the group’s participation in an international system focused on responsible chemical management and resource efficiency.
Aster Textile’s Sustainability Performance in Numbers
Aster Textile tracks its environmental performance through measurable indicators and independent assessment frameworks. Key results from 2025 include:
- Higg FEM score of 71.7: The average verified Higg Facility Environmental Module score across all Aster locations rose from 21.3 in 2020 to 71.7 in 2025.
- 100% renewable electricity: Since 2021, all electricity has been sourced from renewable sources certified through I-REC (International Renewable Energy Certificates), reducing total Scope 1 and Scope 2 greenhouse gas emissions by 50%.
- On-site solar generation: Rooftop solar installations with a total capacity of 4 MW at the Tokat-Erbaa and Artesa Fabrics facilities generated 27% of the group’s total electricity consumption in 2025 and 55% of Aster Textile’s.
- 85% wastewater recovery: Artesa Fabrics’ wastewater treatment plant enables the recovery of 85% of its wastewater.
- 83% certified materials: The share of certified preferred materials in collections and orders increased from 5% in 2020 to 83% in 2025.
- Science-based targets: Aster has set near-term and net-zero science-based targets and initiated the SBTi validation process.
In Artesa Fabrics’ dyehouse, energy, water and chemical consumption are monitored in real time on a machine basis. All chemicals are sourced from positive chemical lists, water-based auxiliary chemicals are preferred, and the chemical inventory is shared transparently through ZDHC InCheck reporting.
Circularity and Product Transparency
Aster Textile’s circular economy initiatives include the 2ND Life Movement, which since 2019 has given waste from its operations a second life in yarns, fabrics and accessories, and a pilot of Resortecs SmartStitch technology, which uses heat-dissolvable thread to make garment disassembly and recycling easier.
Product traceability is supported by systems such as TextileGenesis and TrusTrace, and the company is also building Digital Product Passport (DPP) infrastructure to support product-level transparency in line with upcoming EU requirements.
Aster's vertically integrated manufacturing approach supports coordination between fabric development and garment production, helping different stages of manufacturing work together.
Through its production expertise and sustainability practices, Aster Textile aims to support international fashion brands in meeting expectations for quality, responsible sourcing and transparency.
Frequently Asked Questions About Sustainable Clothing Manufacturing
What is sustainable clothing manufacturing?
Sustainable clothing manufacturing is an approach to garment production that aims to reduce environmental and social impacts through responsible materials, efficient resource management, waste reduction, chemical controls and ethical labor practices.
What fabrics are used in sustainable clothing manufacturing?
Organic cotton, recycled polyester, recycled cotton, hemp, linen and appropriately produced lyocell are among the materials that may be considered. Their environmental performance depends on sourcing and manufacturing conditions.
What are low-impact textile dyeing methods?
Low-water dyeing, certain waterless dyeing technologies, digital textile printing and enzymatic treatments are among the methods evaluated to reduce environmental impacts. Their suitability depends on fabric types and production requirements.
What certifications are important for sustainable textile manufacturing?
GOTS, GRS and OEKO-TEX® STANDARD 100 address different aspects of textile processing and product safety. ISO 14001 focuses on environmental management, while ISO 45001 addresses occupational health and safety management.
How can sustainable clothing manufacturing reduce environmental impacts?
Improving water and energy efficiency, reducing material waste, selecting responsibly sourced materials and managing chemical risks can contribute to reducing environmental impacts.
How can fashion brands evaluate sustainable clothing manufacturers?
Fashion brands can evaluate material sourcing practices, production capabilities, certifications, environmental performance data and working conditions. Manufacturing location, production capacity and quality management are also relevant considerations.
Conclusion
Sustainable clothing manufacturing requires a comprehensive approach that considers material selection, production technologies, resource efficiency and ethical working conditions.
Low-impact dyeing methods, waste reduction, responsible chemical management and energy efficiency can contribute to reducing the environmental impacts of textile manufacturing.
Through its vertically integrated fabric-to-garment approach, international certifications, bluesign® System Partner status and measurable environmental performance, Aster Textile incorporates responsible manufacturing practices into its operations to support international fashion brands.